
Categories List
Recent Posts
 CNWINNEX Unitary Explosion-Proof Air Conditioning Unit | ATEX Certified Energy-Saving Explosion-Proof HVAC for Industrial Hazardous AreasCNWINNEX unitary explosion-proof air conditioning unit is a professional explosion-proof HVAC equipment independently developed by CNWINNEX with cutting-edge HVAC technology and years of in-depth research on high-risk industrial scenarios. Adhering to the design philosophy of safety, energy saving, environmental protection and health, the unit features reasonable overall structure, compact size, light weight, low noise, stable operation and high energy efficiency. It is a mainstream high-demand explosion-proof temperature control device and maintains high Google search popularity in the global industrial explosion-proof HVAC field.
 Explosion-Proof Split Wall Mounted Air Conditioners Delivered to Indonesia Client") CNWINNEX BKT-5.0(F) Explosion-Proof Split Wall Mounted Air Conditioners Delivered to Indonesia ClientRecently, CNWINNEX has completed production, explosion-proof inspection, packaging and shipment. A total of 3 units of BKT-5.0 (F) explosion-proof split wall mounted air conditioners were successfully delivered to a client in Indonesia to provide safe and reliable temperature control solutions for local high-risk industrial areas.
 CNWINNEX ATEX Certified Explosion Proof Combined Air Handling Unit, Modular Explosion-Proof AHU for Hazardous AreasDiscover CNWINNEX ATEX certified explosion-proof modular air handling units for Zone 1 and Zone 2 hazardous areas. Configurable AHU sections provide safe ventilation, filtration, cooling, heating and air treatment for chemical, oil and gas, pharmaceutical and energy storage facilities.
 CNWINNEX BKT Series 316L Stainless Steel Explosion-Proof Window AC Delivered to Petrobras Offshore Drilling Platform Project in BrazilRecently, a new batch of CNWINNEX explosion-proof window air conditioners has completed factory explosion-proof verification, anti-corrosion inspection and packaging, and been successfully delivered to a Brazilian client. The units will be officially applied to the hazardous area temperature control project of Petrobras offshore drilling platforms in Brazil. The shipment includes 2 units of BKT-7.5 explosion-proof window air conditioners (7.5KW cooling capacity) and 1 unit of BKT-2.6 explosion-proof window air conditioner (2.6KW cooling capacity). Built with full 316L stainless steel enclosure and customized with a 60Hz power system to meet the on-site power conditions of offshore drilling platforms, the units deliver outstanding salt spray resistance and anti-corrosion performance, serving as fully ATEX Certified professional explosion-proof HVAC solutions for offshore drilling platform working conditions.
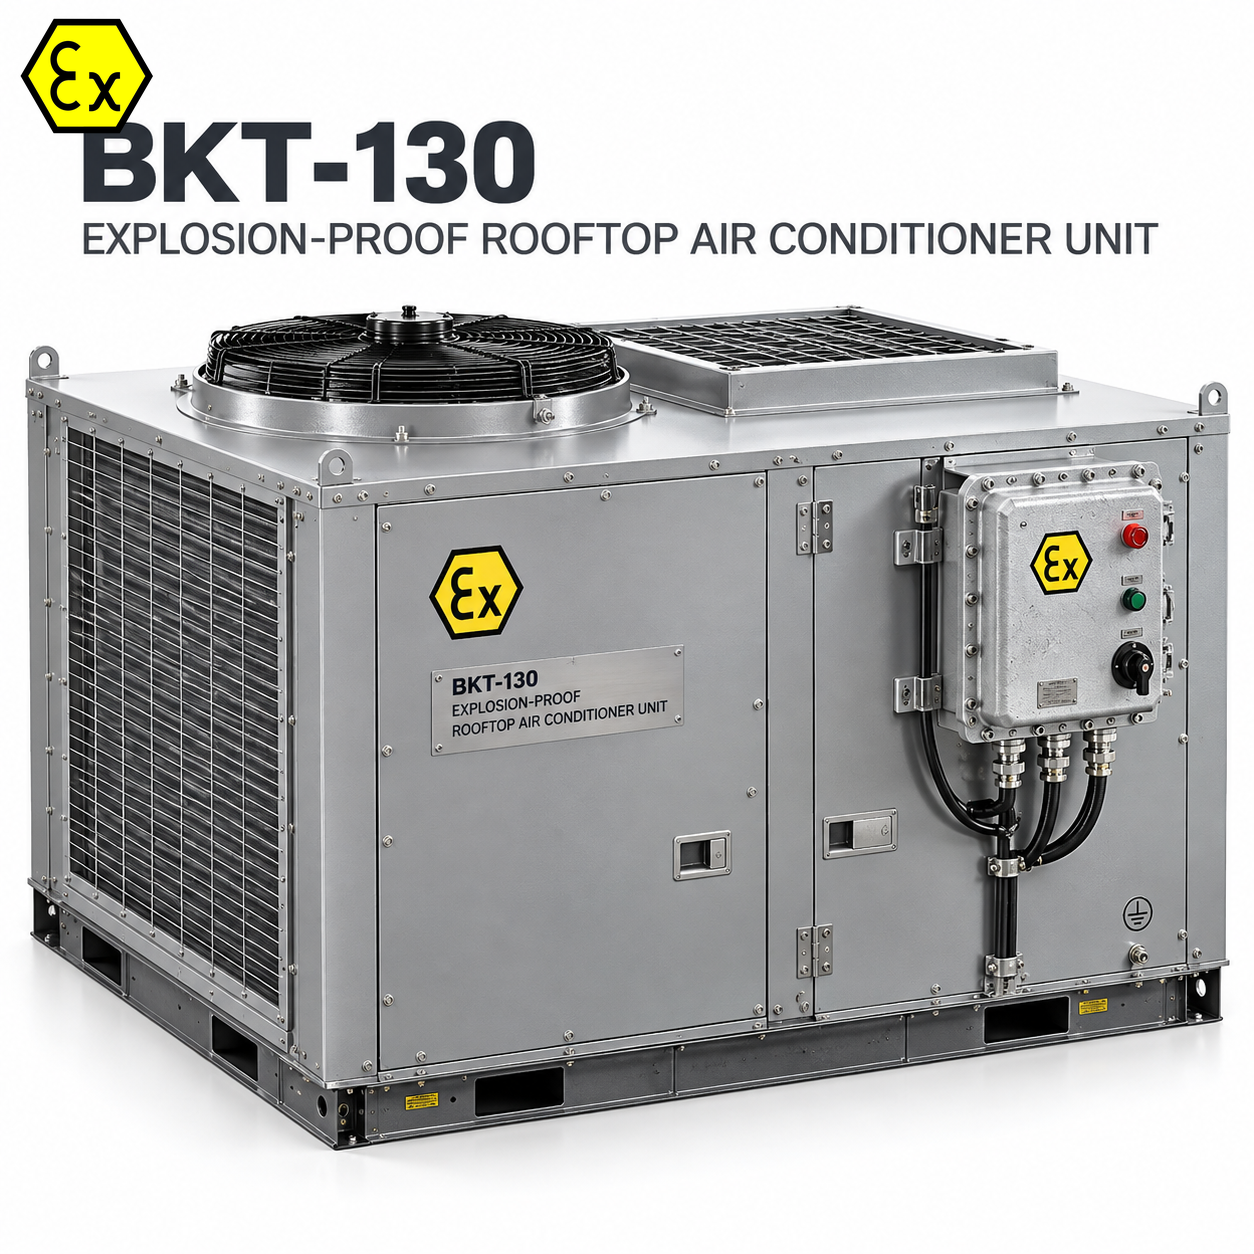
 BKT-130 Explosion Proof Rooftop Air Conditioning Unit | ATEX / CNEX Certified Packaged Rooftop HVAC for Hazardous AreasCNWINNEX BKT-130 explosion proof rooftop air conditioning unit is a fully packaged rooftop HVAC system integrating cooling, heating and 100% fresh air supply. The whole unit is fully explosion-proof engineered for industrial sites with explosive gas and dust atmospheres. For chemical, oil & gas, pharmaceutical and hazardous material projects, **explosion proof rooftop air conditioner** is a widely searched hazardous-area climate control solution. The all-in-one rooftop design minimizes on-site ductwork installation and delivers centralized fresh air and temperature control for large industrial workshops.
 Why Choose CNWINNEX Explosion Proof Air Conditioners | Full-Range Explosion-Proof HVAC for Global Hazardous Industrial ProjectsIn hazardous locations such as petrochemical plants, oil and gas facilities, pharmaceutical sites, LNG terminals and offshore platforms, conventional air conditioners carry potential ignition risks. Certified explosion-proof air conditioning is essential for protecting personnel, precision instruments and continuous production operations.
CNWINNEX has accumulated extensive experience in explosion-proof HVAC solutions. We offer a complete explosion-proof air conditioner portfolio to meet international certification requirements, site conditions and customized demands for global projects. Our products have been successfully exported to the USA, United Kingdom, Brazil, Argentina, Indonesia, Singapore, Vietnam, Thailand, Malaysia, UAE, Qatar, Uzbekistan and Australia. ATEX Split Wall-Mounted Explosion-Proof Air Conditioners to UAE for Middle East Oil & Gas Project") CNWINNEX Ships 2 Sets of 5.0KW (2HP) ATEX Split Wall-Mounted Explosion-Proof Air Conditioners to UAE for Middle East Oil & Gas ProjectRecently, CNWINNEX has completed factory quality inspection, explosion-proof verification and packaging for 2 sets of 5.0KW (2HP) ATEX split wall-mounted explosion-proof air conditioners. The equipment was exported to the United Arab Emirates via air freight to ensure rapid delivery and on-time commissioning of the overseas project. These high-precision explosion-proof air conditioners will be applied to temperature control of instrument rooms in Zone 1 hazardous areas for local oil and gas chemical projects in the UAE, ensuring stable operation of equipment and safe production in high-risk working conditions. This delivery marks another benchmark order of CNWINNEX high-end ATEX-certified explosion-proof temperature control equipment in the Middle East market.
 CNWINNEX Explosion-Proof HVAC Unit for Pressurized RoomsCNWINNEX explosion-proof HVAC unit integrates cooling, heating, dehumidification, ventilation and indoor positive pressure maintenance. It features reliable explosion-proof performance, compact and neat appearance. Enclosure options include SS304, SS316L stainless steel and powder-coated carbon steel, suitable for corrosive gas and high-humidity sites. Various models with broad cooling capacity range, fully assembled before delivery and available for project customization.
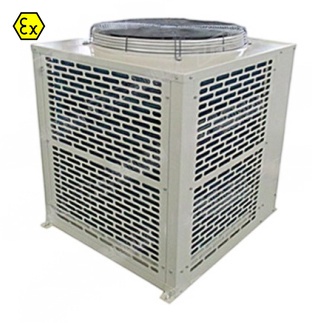
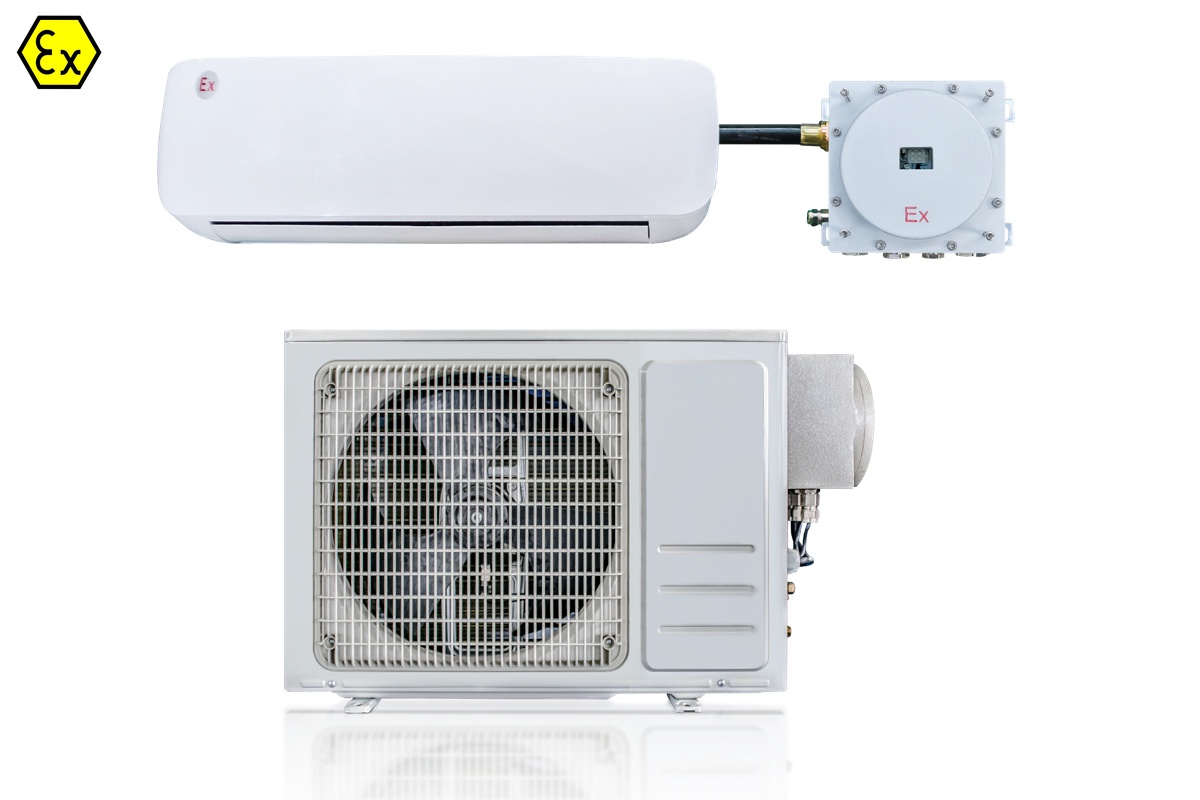
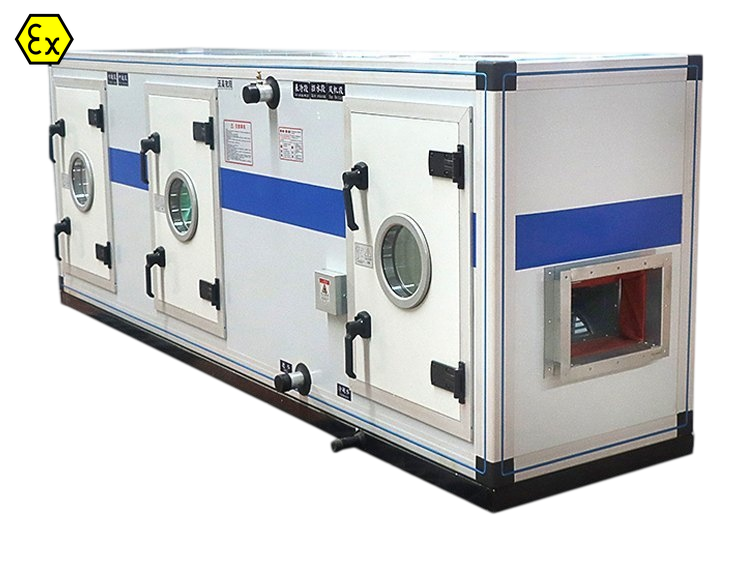
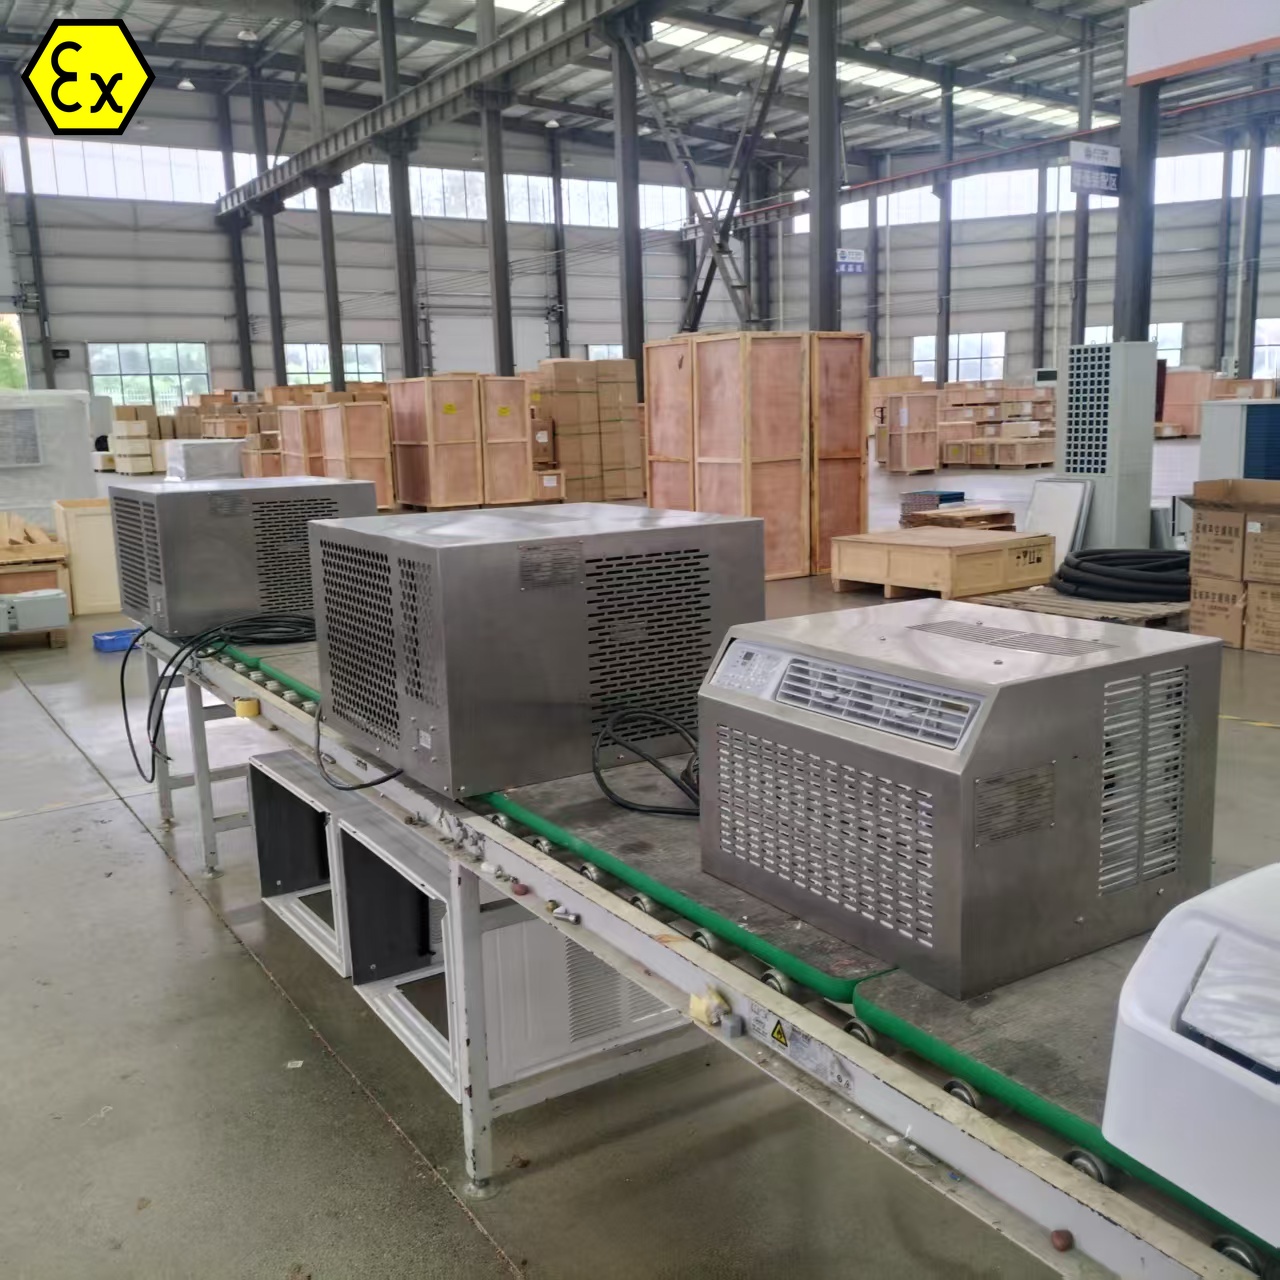
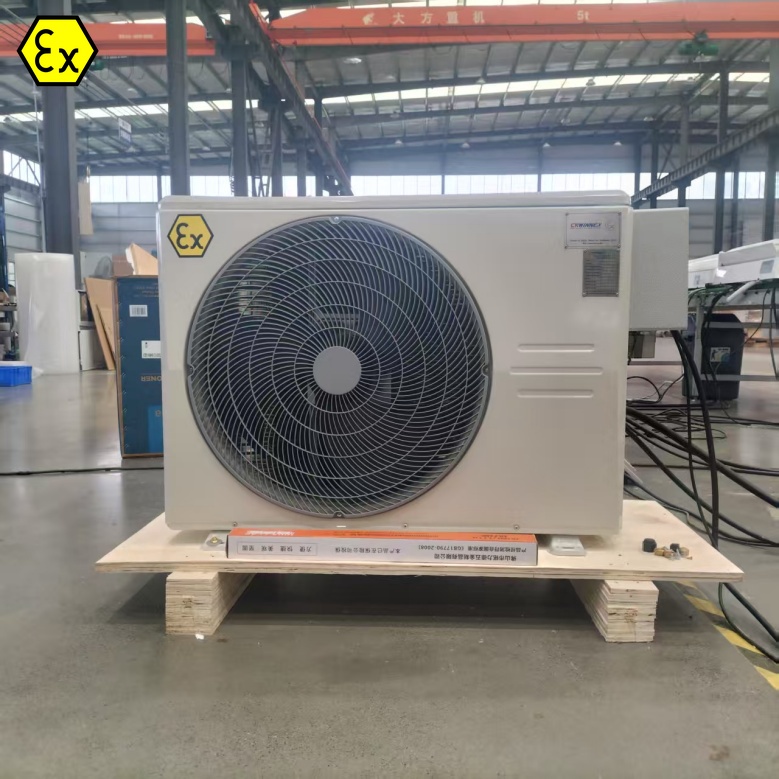

CNWINNEX Unitary Explosion-Proof Air Conditioning Unit | ATEX Certified Energy-Saving Explosion-Proof HVAC for Industrial Hazardous Areas
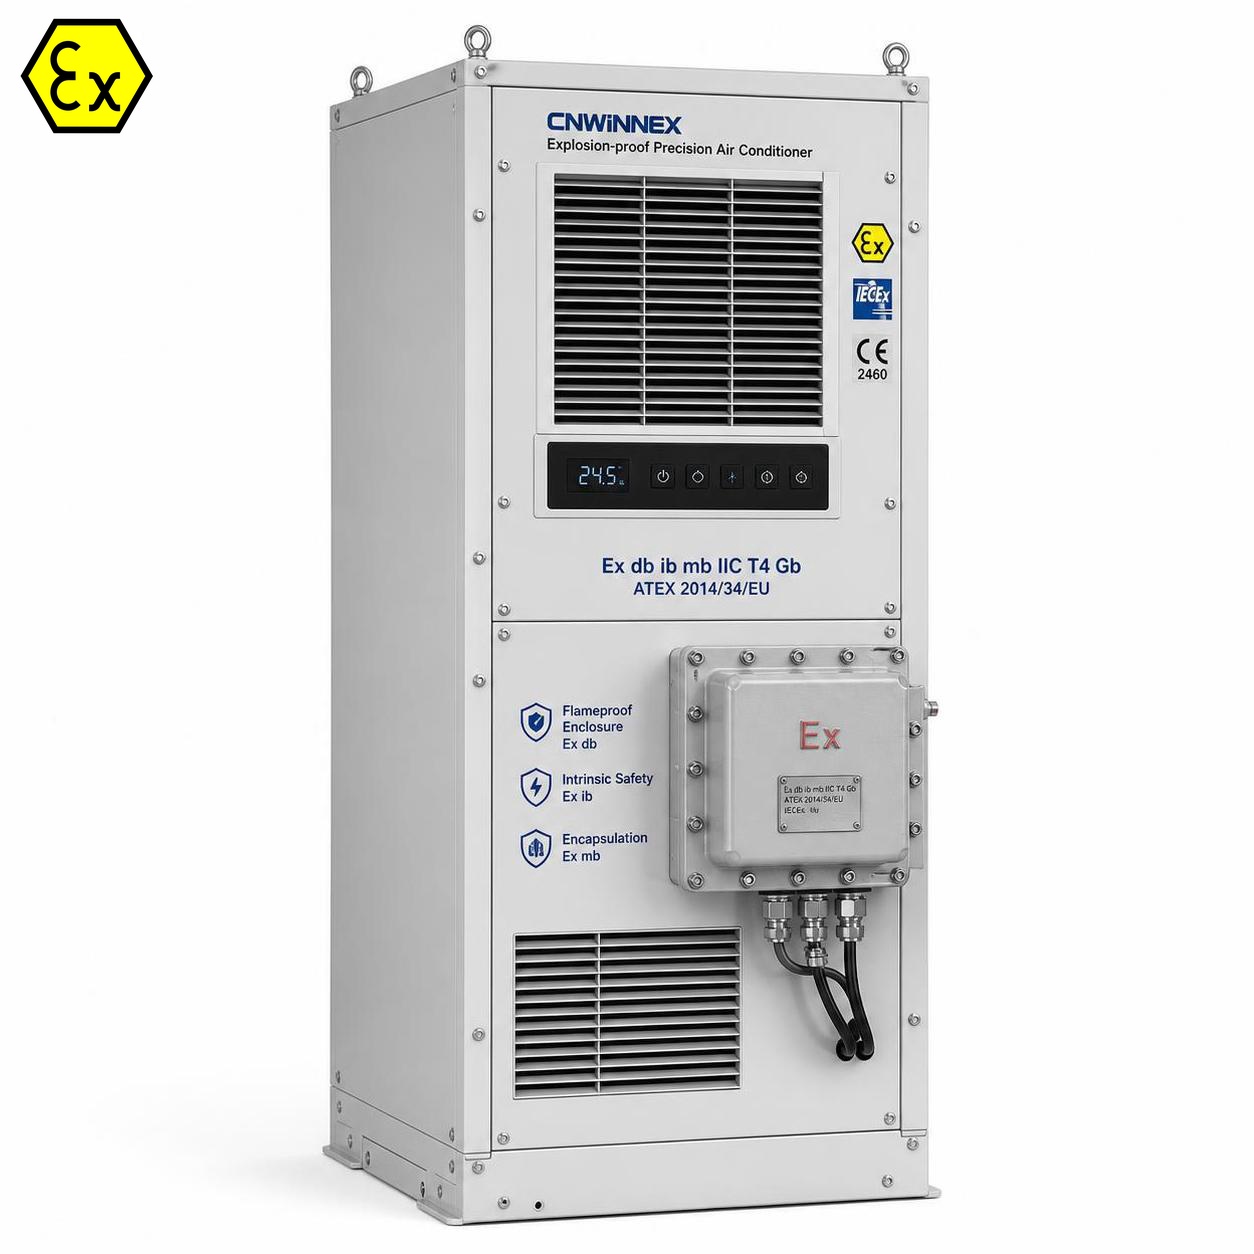
CNWINNEX unitary explosion-proof air conditioning unit is a professional explosion-proof HVAC equipment independently developed by CNWINNEX with cutting-edge HVAC technology and years of in-depth research on high-risk industrial scenarios. Adhering to the design philosophy of safety, energy saving, environmental protection and health, the unit features reasonable overall structure, compact size, light weight, low noise, stable operation and high energy efficiency. It is a mainstream high-demand explosion-proof temperature control device and maintains high Google search popularity in the global industrial explosion-proof HVAC field.
Manufactured in strict accordance with ATEX Directive 2014/34/EU and EN 60079 international explosion-proof standards, all units are fully ATEX Certified. Official explosion-proof marking: Ex db ib mb IIC T4 Gb. It is suitable for hazardous areas with IIA, IIB, IIC class and T1~T4 group flammable gas and vapor mixtures, covering Zone 1 and Zone 2 explosive atmospheres. The product fully complies with strict HSE management and acceptance standards for global chemical, oil & gas, pharmaceutical and energy storage projects.
Core Product Advantages & Specifications
1. High-Efficiency Scroll Compressor with High EER
Equipped with high-EER hermetic scroll compressor, the unit delivers strong power, lower energy consumption and ultra-low failure rate. The optimized seasonal energy efficiency ratio ensures stable full-year operation and remarkable long-term economic benefits for industrial sites.
2. Multi-Functional Integrated Design
Integrates air supply, cooling, heating, dehumidification and air purification functions in one unit. It comprehensively solves industrial environmental problems such as high temperature, humidity, turbid air and peculiar smell, improving the safety and comfort of high-risk working environments.
3. Premium Brand Components for Stable Performance
Adopts high-quality brand-name refrigeration, electrical and control components. With strict factory explosion-proof inspection and working condition simulation tests, the unit features stable performance, low maintenance cost and high cost-effectiveness for long-term high-intensity industrial operation.
4. Intelligent Dynamic Control for Full-Year Adaptation
Equipped with advanced intelligent control technology and optimized dynamic temperature control model, the unit automatically adjusts operating modes according to seasonal temperature and load changes, adapting to complex full-year working conditions and improving overall energy efficiency.
5. Complete Model Coverage & Customization Support
Available in air-cooled, water-cooled and air-cooled heat pump types, with a cooling capacity range of 20kW to 200kW to match industrial sites of all sizes. Heating options include electric heating, hot water heating and steam heating. Custom special models with partial fresh air, 100% fresh air, high temperature, low temperature and dual cold source are available for personalized project demands.
6. High-Density Thermal Insulation Structure
Adopts special high-density thermal insulation panels for air conditioners, featuring excellent heat insulation performance and ultra-low air leakage rate, reducing cold and heat loss and improving overall heat exchange efficiency.
7. Multiple Safety Protection Functions
Built-in multiple intelligent protection functions including overload, overvoltage, overheat, phase loss and leakage protection. Combined with full-circuit explosion-proof structure design, it completely avoids equipment failure and ignition risks, ensuring ultra-high operational safety and reliability.
8. Eco-Friendly Refrigerant Options
Optional environmentally friendly refrigerants: R22, R407C and R134a. Adopting advanced production and sealing technology to achieve zero refrigerant leakage during operation, meeting global industrial environmental protection standards and overseas market access requirements.
Widely used in petroleum, chemical, oil & gas exploitation, fine pharmaceutical, new energy energy storage, hazardous material warehousing, coating workshops and other Zone1/Zone2 high-risk industrial areas with flammable and explosive gas or vapor atmospheres worldwide.
Leave A Reply
Please give us a message